
Coating process
Our first initial meeting will be to determine your colors and design.
After our first meeting, the following is a brief explanation of how we go about Cerakoting your firearm.
Your firearm is received in our shop and examined to make sure it is in safe working order. Once it is determined that it is indeed in safe working order then it is taken to step 2, If it is not in safe working order it is returned to the customer to have it properly repaired by a gunsmith before we can take on the job. We do have access to a couple licensed gunsmiths if you want us to have the gun repaired for you.
In step 2 the firearm is completely disassembled ( every last pin, nut, screw, and spring ) If the weapon has a barrel that is attached to the weapon it must be removed as well. If the barrel is not removed and the customer requests that the barrel not be removed they must sign a waiver stating so as we are not responsible for the adhesiveness of the Cerakote to that part of the weapon. We then examine each part and make notes of any problems that we see that may need to be addressed before the firearm is coated, we then contact the customer to those problems that we see so they can decide how to continue. If all parts are in good working and safe order then we continue on to step 3. Please note that some parts for example the front sights on some firearms will need to be replaced because from the factory they are either not reusable, or so extremely tight that they can be easily broken, chipped, or damaged. We will take great care in disassembly of your firearm, but things do happen from time to time that are beyond our control.
WE ARE NOT RESPONSIBLE FOR DAMAGE TO A SIGHT DURING REMOVAL.All parts that will be coated are then given an acetone bath to remove all oil, grease and dirt.
Cerakote is applied extremely light in order to not make problems with tight tolerances, That said I typically mask off pins and only shoot the heads of the pins. If you want the full pin coated you need to verify this at the time of drop off and you need to realize that you may or may not have a problem installing the pins. You may have to take some steel wool and gun lube to the outside area of the pin in order to make it fit correctly in those tight tolerance instances. We can also at request plug any holes you may wish to have plugged. Also if there are any places on the gun that you know for a fact that there will be a tolerance problem you need to let us know beforehand so we can either mask this area off or arrange for just a dusting of the coating on that area.
Markings: As for markings anything that is painted or lightly laser etched will be lost during the cleaning and coating process. There is no way to save these markings. I have been asked about replacing these markings via model car type paint as seen on youtube. You can do this yourself very easily via this video We will not do it here because we cannot guarantee the success of the color fill and how long it will last before flaking off. This does work well but in most cases you will need to reapply it over time. You need to remember that Cerakote is designed not to allow other things to stick to it very well.
Serial numbers will be masked at no additional charge when necessary. When not necessary we will coat over them as long as they can be plainly read through the coating.
We then sand blast all parts to be coated with Cerakote with a very fine aluminum oxide media to remove all coatings from all pieces and to give the Cerakote a clean surface to adhere to.
Each part is then taken to the coating prep area to be hung for coating. Once all parts are hung properly they are then examined once more before coating is applied to make sure all the parts are cleaned and prepped correctly and ready for a successful coating of Cerakote to be applied.
The parts rack is wheeled into the Coating booth immediately after proper prep is completed to minimize the time for contamination to occur between hanging and coating. Each part is sprayed via Cerakote’s rigorous standards using equipment and technique specified by Cerakote.
After the Cerakote coating is applied the parts are taken to our baking oven to bake out to Cerakote Standards. If there is any stenciling to be done the parts that require the stencil will be flashed out as required, removed from the oven stencils applied and the correct color applied, then replaced into the oven for the final bake out.
After the parts are baked out they are removed from the oven and cooled. The parts are then inspected for proper coating thickness, look, and feel. If the parts are labeled as good they are taken to our reassembly area where the firearm is then reassembled for the return to the customer. If any of the parts is determined not to pass our quality standards they are taken back to step 3 to start the process all over again.
Note: It is recommended that the firearm not be used for approximately 3 days following coating in order to allow the Cerakote to fully harden.
If you have any questions concerning the Cerakote Application process please feel free to give us a call or drop us an email to discuss. If we don’t know the answer we know the correct people to talk to at Cerakote to find the answer for you.
Coating Series Info
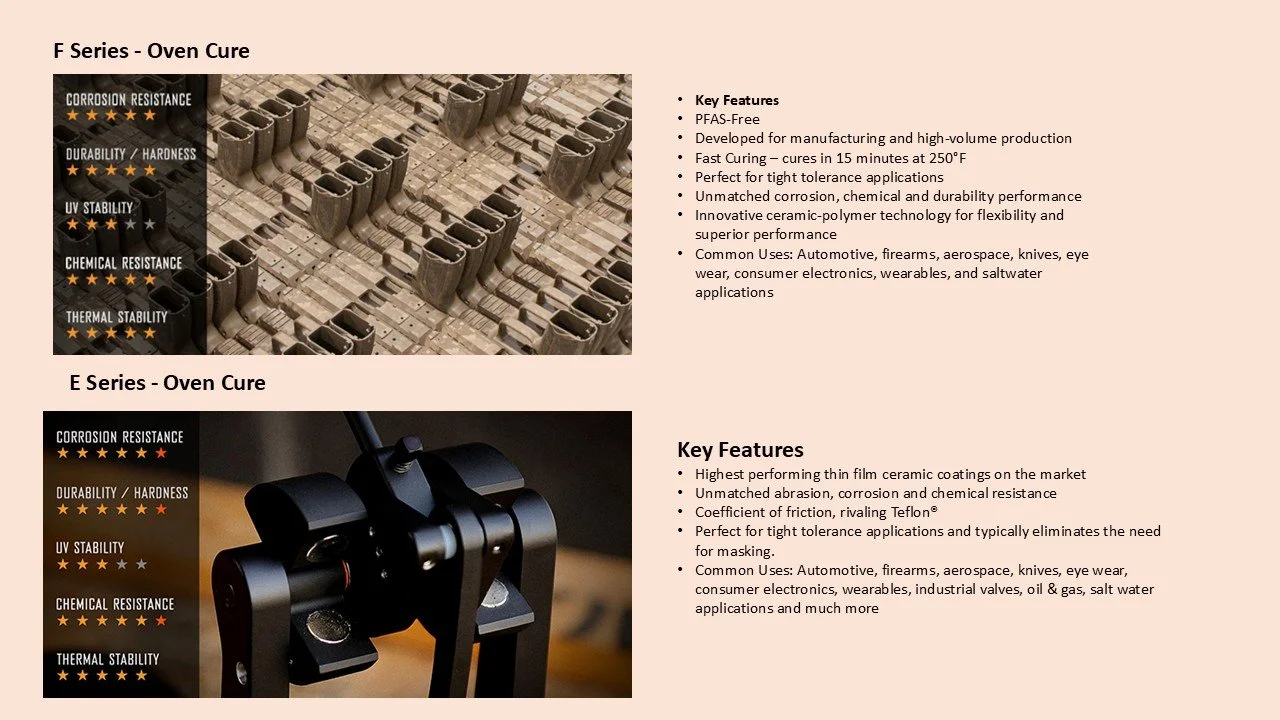
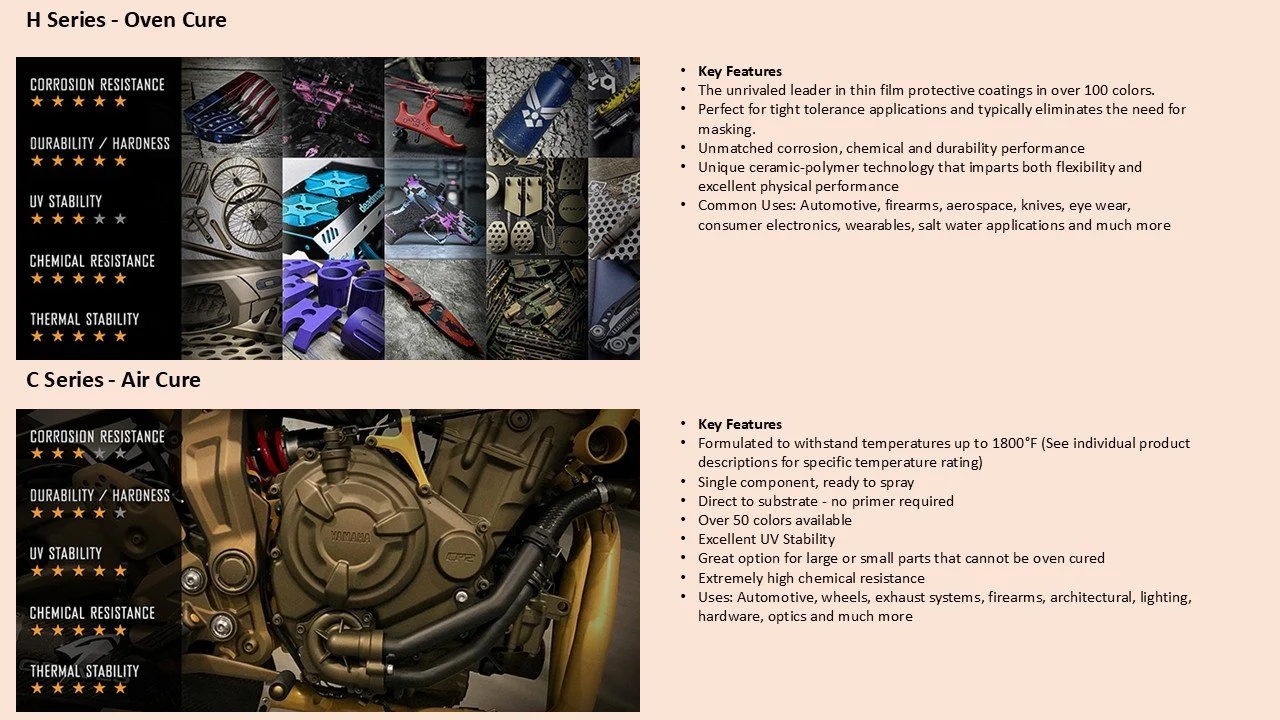
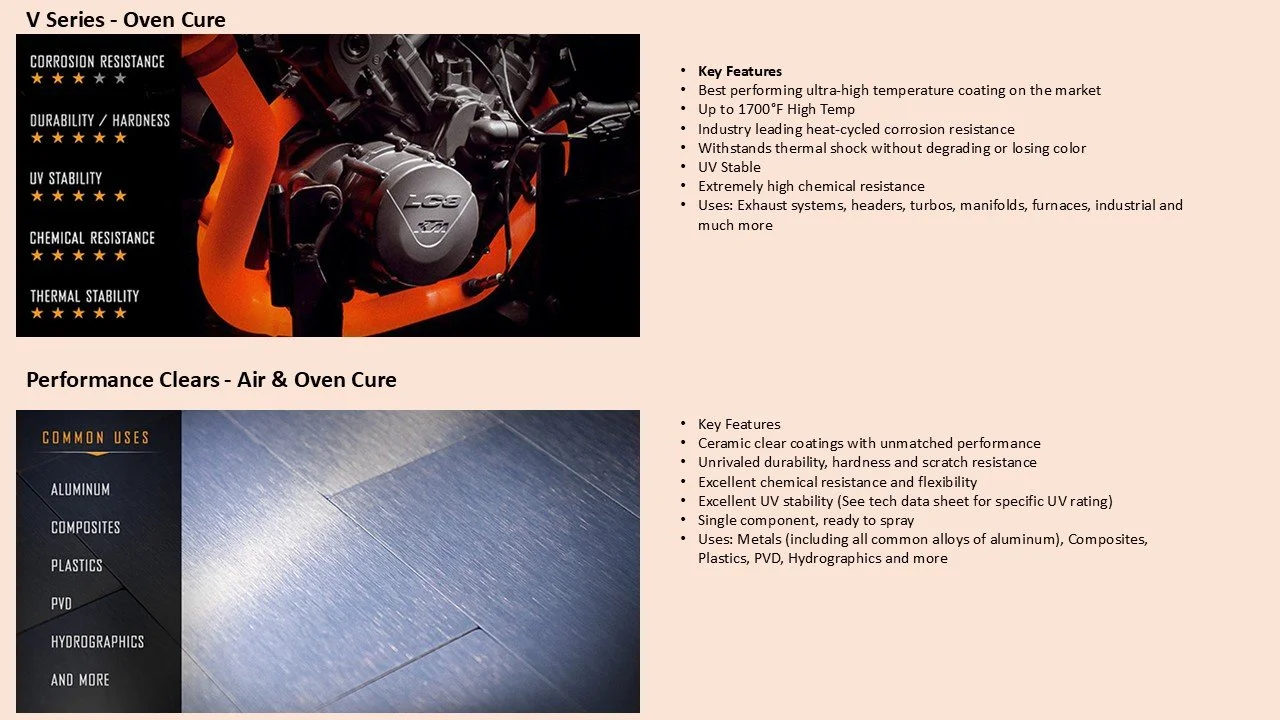
Please I ask anyone dropping off a firearm for Cerakote to clean the firearm of all dirt and grit prior to bringing it in, dirty firearms destroy the Acetone in the degreasing tank causing the Acetone to be useless. If your firearm is dirty we will automatically charge you a cleaning fee of $75 so we don’t have to replace acetone after every use.
Disassembly / Reassembly Is always on top of the Cerakote® coating prices.
It usually ranges between $45 – $125 depending on the Gun and difficulty.
Although some… Such as the Springfield XD – $200 and the Springfield XDM – $250
So if your worried about your firearm please Call for accurate pricing.
Cerakote® colors that we do not normally stock will add an additional $35 to your order
Tight Tolerance Parts and Markings:
We do not coat sears, springs, bores/chambers or other tolerance critical or high-flex parts. In addition, we do not media blast scopes or other optics and, as a result, there will not be as good an adhesion of the Cerakote to those items.
TOLERANCE: For standard firearms applications it is often inadvisable to coat both pins and pin holes, as the resulting one (1) mil thickness of the coating when applied to rounded surfaces creates increase of two (2) mil to the part tolerance and four (4) mil (.004) when both hole and pin are coated. This is also applicable to auto-pistol slide and frame fit, such as on tight-fitting 1911’s. We typically plug or mask holes and pins and only coat the pin ends. However, we can coat pins and holes and then custom fit these parts after coating for an additional charge. We recommend hand fitting and lapping for 1911 pistol slides and frames as this will yield a precision fit and can help to tighten looser fitting slide/frame combos.
MARKINGS: For receivers, frames, slides, Picatinny rails which have painted on or lightly laser etched markings these markings will be lost during the surface preparation and coating unless they are machine engraved or stamped. If these markings are of great importance we can mask over them, but those areas in and immediately around the markings will not be coated and, as such, will not blend. Manufacturer’s serial numbers will be masked at no additional charge where needed or coated where possible. Some manufacturer model numbers, name etc which are laser engraved will be masked over. This is per BATFE (ATF) regulations. Please consult us for specific requirements.
CERAKOTE STANDARD PERFORMANCE METRICS:
RUST RESISTANCE: Cerakote™ finishes have been tested in salt spray and full emersion and have withstood beyond 3,000 hours in salt spray and hundreds of hours in full emersion testing. These results outperform other finishes by over 10x. This makes Cerakote™ finishes the clear choice for marine environments and other environments subject to high humidity and salt water environments.
WEAR RESISTANCE: Cerakote™ finishes can withstand over 5,000 (5,212) wear cycles per mil (.0001). The Tabor wear test uses an 8″ abrasive wheel applied to a metal plate coated with 1 mil thickness of the Cerakote coating. In addition, Cerakote’s Coefficient of Friction is 80% less than stainless steel against stainless steel. So, when one or both moving parts of a firearm are coated you can expect a significantly longer product duty cycle or service life.
ADHESION: Cerakote finishes have an ASTM D3359 rating of 5B and can withstand a 180° mandrel bend rotation test around a 1/4″ mandrel and a ball bearing impact test of 160 inch-lbs with no cracking or loss of adhesion. This is significant performance given Cerakote’s 9H pencil hardness, which is the highest hardness rating in the scale.
HARDNESS AND SCRATCH RESISTANCE: ASTM D3363 is a 9H pencil hardness and 6H scratch resistance.
FILM THICKNESS: 1.0 mil or less, depending on coating series used.
Got a Question? Email us at akctknives@gmail.com